Five years ago, I emptied my savings account to launch a small-scale biomass pellet factory—no prior industry experience, just a vague idea that biofuels were the future. I made the dumbest call possible: I bought a cheap “all-in-one production line” from a local vendor who promised it’d be “plug-and-play.” Within 90 days, I was drowning in crises: mold clogs grinding production to a halt, environmental inspectors issuing warnings that left me up at night, and raw material transport bills that ate into every penny of potential profit. That brutal wake-up call drilled one truth into me: cost-effective biomass pellet production line design for small businesses is the make-or-break for any pellet factory—not how little you spend on equipment. Today, with my factory churning out 5,000 tons annually, I’m sharing every hard-earned lesson I’ve learned—no fluff, just the real pain points and how I fixed them.
Why Most Beginners Fail at Production Line Design
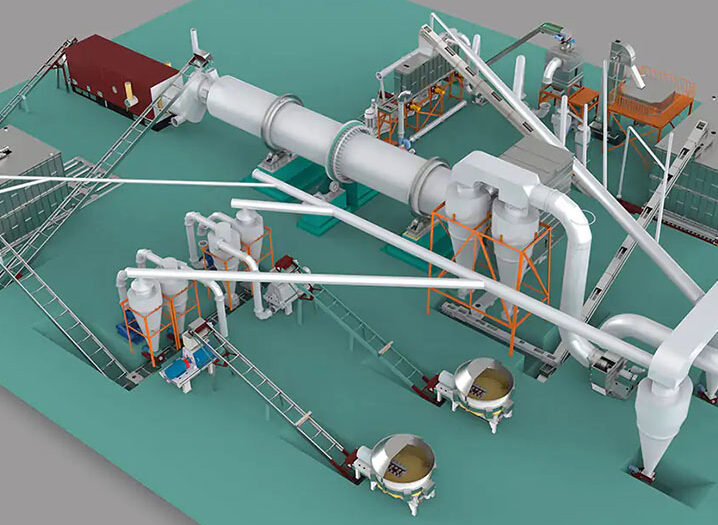
Like most newbies, I fixated on cutting equipment costs instead of building a cohesive system. I thought a production line was just a crusher, pellet mill, and cooler strung together—how hard could it be? Spoiler: It’s a delicate ecosystem that ties together biomass raw material pretreatment for pellet production, granulation, compliance, and bottom-line math. After talking to 50+ fellow entrepreneurs (many of whom folded within a year), I saw three deadly design mistakes repeat over and over:
- Ignoring raw material characteristics: I tried using the same mold for sawdust, straw, and coconut shell at first—big mistake. It led to abysmal biomass pellet molding rate optimization, with half the pellets crumbling and the mill jamming every few hours. You can’t force one-size-fits-all equipment on finicky raw materials.
- Underinvesting in environmental protection equipment: Skimping on dust removal systems results in failed EIA compliance for small-scale biomass pellet factories and forced shutdowns, which are far more costly than proper equipment.
- Unreasonable site and process layout: Poor workflow design increases labor costs by 30% and reduces production efficiency by 20%.
The good news? These mistakes aren’t inevitable. I’m breaking down the core parts of a solid biomass pellet production line—rooted in my own failures and wins, not just textbook advice—to help you build something that lasts.
Core Components of Biomass Pellet Production Line Design
A production line that works isn’t generic—it’s built around your raw materials, how much you want to produce, and local rules. Below, I’m walking through each critical section with the fixes that turned my failing factory around.
1. Raw Material Pretreatment System: The Foundation of Stable Production
Raw materials are everything—mess up their pretreatment, and you’ll fight quality and equipment issues daily. My first factory tanked because I skipped proper drying, thinking I could save money by letting raw materials “air out.” The result? 20% of my pellets were loose, powdery, and unsellable. I quickly learned biomass raw material drying for pellet production isn’t a luxury—it’s non-negotiable.
Key Design Points:
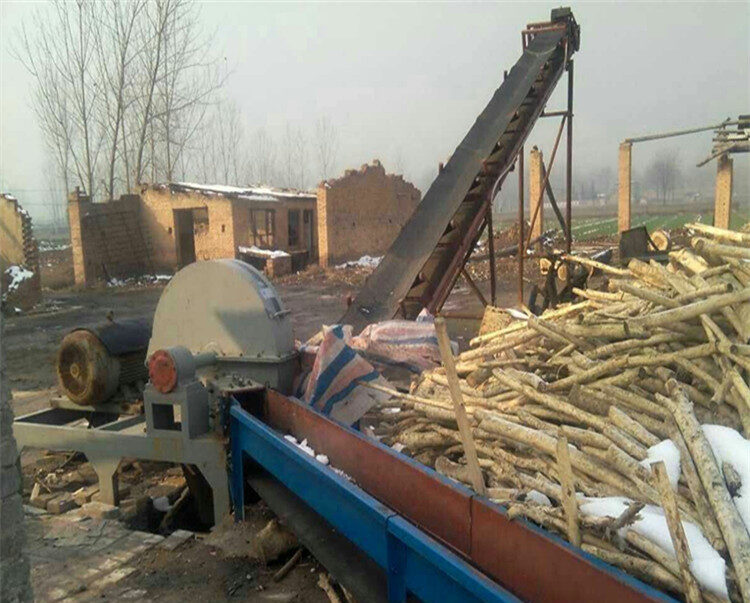
- Crushing Module: Raw materials need to be 5mm or smaller to granulate smoothly—anything bigger clogs the mill. For hardwood sawdust, I swear by a hammer mill for hardwood sawdust pellet production with a 4mm screen mesh; it chews through dense wood without bogging down. Straw’s trickier—go for a double-shaft shredder to tackle those tough fibers. And don’t skip an iron removal device! I learned this the hard way when a stray nail destroyed my mill’s roller—costing me $1,200 and 2 days of downtime. This tiny add-on has saved me thousands since.
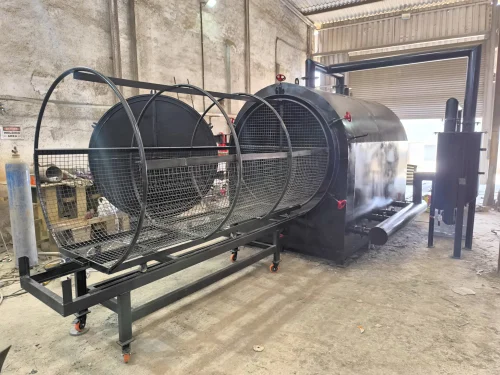
- Drying System: Aim for 12-15% moisture content—you can test this by squeezing raw materials: no clumping, just a dry feel. My first dryer was a cheap small hot air model that guzzled electricity and left moisture all over the place. I upgraded to a triple-barrel rotary dryer for biomass pellets paired with a biomass hot air furnace, and my energy bills dropped 40% overnight. If you’re doing less than 5 tons a day, a batch-type dryer for small biomass pellet plants is more budget-friendly—just don’t skimp on temperature controls.
- Storage and Conveying: Build a moisture-proof warehouse with dehumidifiers—I spent $4,500 on a 200㎡ steel structure, and it’s prevented hundreds of tons of raw materials from getting damp (damp materials = mold = lost money). Keep conveying distances short: bucket elevators cut my labor costs by 25% compared to manual hauling, and they’re way less error-prone.
My Pain Point Solution: I once ran out of raw materials mid-harvest season because I didn’t lock in suppliers. Now, I sign village-wide contracts with a 10% advance payment—that guarantees a steady stream of agricultural waste raw material for biomass pellets. I also cap transport at 15 kilometers—any farther, and fuel costs eat into profits faster than you’d think (I learned this after a 20km haul made a whole batch unprofitable).

2. Granulation System: The Core of Production Efficiency
The pellet mill is your factory’s heart—get it wrong, and you’ll be stuck fixing breakdowns instead of making money. I blew $12,000 on a shoddy flat die pellet mill early on; it overheated after 4 hours of use, and the vendor ghosted me when I asked for repairs. That’s when I realized high-quality biomass pellet production starts with the right mill.
Key Design Points:
- Equipment Selection: For industrial use, a ring die pellet mill for biomass production is non-negotiable—it’s way more stable and efficient than flat die models. My current Chang sheng KLS420 (90kW motor) cranks out 1.5 tons an hour, even with mixed sawdust and straw. The biggest tip? Find a manufacturer that offers a custom compression ratio ring die pellet mill for biomass. Different materials need different ratios (5-12:1)—coconut shell needs 10-12:1 for dense pellets, while softwood sawdust works with 5-8:1. Don’t settle for a one-ratio-fits-all mold.
- Mold and Roller Maintenance: Use Cr12MoV molds (hardness ≥58HRC)—they last 800-1000 hours, which is double the lifespan of cheaper molds. Cr12MoV mold maintenance for pellet mills is simple: clean them daily, lubricate regularly, and keep spares on hand. I once had a mold clog and had to shut down for 3 days—losing $2,300 in profits. Now, I train my team to do basic mold repairs; it’s saved us countless headaches.
- Temperature and Pressure Control: Keep mold temperature between 85-95℃—too cold, pellets won’t bind; too hot, they carbonize. A PLC control system is worth the investment—it monitors temps and pressure in real time, so you don’t have to stand over the mill 24/7. I cut manual errors by 60% after installing one.
3. Cooling, Screening and Packaging System: Ensure Product Quality
Freshly made pellets are 80-90℃ and fragile—skip proper cooling and screening, and you’ll have broken pellets and angry customers. I once shipped a batch without cooling it properly; 15% broke in transit, and I had to refund the order. That’s when I prioritizedbiomass pellet product quality assurance in this step.
Key Design Points:
- Cooling Module: A counterflow cooler for biomass pellets is a game-changer—it cools pellets to room temp in 15-20 minutes, boosting their strength by 30%. I tried natural cooling at first; it took 3 hours, and pellets absorbed moisture from the air. Don’t waste time with it—invest in a counterflow cooler.
- Screening System: Use a vibrating screen with 6mm and 8mm meshes to sift out unqualified pellets and powder. I reuse the recovered powder—it cuts waste by 5%, which adds up fast. Every little bit of efficiency counts when you’re running a small factory.
- Packaging Equipment: Pick automatic packaging scales based on your customers—25kg bags for retail, ton bags for industrial buyers. I added a finished product hoist last year; it eliminated 2 manual loading jobs and sped up shipping. It paid for itself in 3 months.
4. Environmental Protection and Energy Saving Design: Avoid Shutdown Risks
Environmental compliance isn’t optional—ignore it, and you’ll get shut down. My first factory got hit with a $7,500 fine for excessive dust emissions; I had to halt production for 2 weeks to fix it. It’s a mistake I’ll never make again. Per GB 16297-1996, particulate emissions must meet biomass pellet factory dust emission standards (≤120mg/m³).
Key Design Points:
- Dust Removal System: Install a cyclone and bag filter dust removal for pellet mills—it traps 99% of dust. I spent $1,800 on two pulse dust collectors, and I passed my next EIA inspection on the first try. Fines and downtime cost way more than proper dust removal—don’t cut corners here.
- Noise Control: Neighbors will complain if your factory is too loud. Pick low-noise equipment and add sound insulation cotton—aim for Class 2 noise standards (≤60dB daytime, ≤50dB nighttime). I had a neighbor file a complaint early on; sound insulation fixed it for good.
- Energy Saving Measures: Cut costs with energy-efficient motors and a waste heat recovery system for biomass pellet dryers. I use the dryer’s waste heat to warm the workshop in winter—slicing heating costs by 30%. My line uses 150kWh per ton, which is below the industry average of 180kWh. Every kWh saved boosts your profit margin.

5. Cost-Benefit Analysis Based on Production Capacity
Your production line’s design has to align with your budget and output goals—building something too big (or too small) is a waste. Below is a breakdown of costs and profits based on three common sizes—these numbers come from my own books and conversations with other factory owners, not generic industry reports.
| Production Capacity | Total Investment | Operating Cost per Ton | Profit per Ton | Payback Period |
|---|---|---|---|---|
| 0.5-1 ton/hour (small-scale) | 80,000-180,000 yuan | 430-480 yuan | 200-350 yuan | 6-12 months |
| 1-3 tons/hour (medium-scale) | 200,000-500,000 yuan | 380-420 yuan | 250-400 yuan | 8-14 months |
| 5+ tons/hour (large-scale) | 700,000-1,200,000 yuan | 320-360 yuan | 300-450 yuan | 12-18 months |
Note: These numbers are based on straw and sawdust. Profit varies by location—if you’re in an area with lots of agricultural waste, low-cost raw materials for biomass pellet production can slash your costs by 10-15%. I’m lucky to be near farmland; it’s one of my biggest competitive advantages.
FAQ: Answers to the Most Common Questions from Investors
1. Q: Can I use a mobile production line for raw material collection?
A: Absolutely—I have a friend who uses one, and it cuts his transport costs by 30%. Go for a modular design on a trailer, but make sure it meets local environmental rules. He got a warning once for insufficient dust control; fix that upfront.
2. Q: What’s the best raw material for beginners?
A: Sawdust, hands down. It has low, consistent moisture and a high molding rate—way more forgiving than straw. I tried straw first, and it took me months to get moisture levels right. Start with sawdust, then add other materials later.
3. Q: Do I need a professional EIA report before building the factory?
A: Yes. Complete EIA filing and approval before construction. The environmental protection investment accounts for 4-5% of the total investment, including dust removal, noise control, and waste disposal.
4. Q: How to choose the right compression ratio for the mold?
A: It’s all about your raw material. Softwood sawdust needs 5-8:1, hardwood 8-10:1, and coconut shell/straw 10-12:1. Ask your equipment supplier for a custom mold—most good ones offer this for free if you buy the mill.
5. Q: Can the production line be upgraded later?
A: Yes. Design with expansion in mind—reserve space for adding a second pellet mill and expanding the warehouse. My factory upgraded from 1 ton/hour to 1.5 tons/hour with minimal modification.
6. Q: What’s the main cause of mold blockage?
A: Moisture—if your raw materials are over 18% moisture, they’ll clog the mold fast. Wrong compression ratio is the other culprit. I clean my mold every night after production; it prevents buildup and blockages.
7. Q: How many laborers are needed for a 1.5-ton/hour line?
A: 3-4 people with PLC automatic control—1 for raw material feeding, 1 for equipment monitoring, 1-2 for packaging and loading.
8. Q: Are there government subsidies for biomass pellet factories?
A: Yes—they’re a huge help for new factories. I get $6-$12 per ton for straw utilization and energy-efficient equipment. Check with your local agricultural and environmental offices—each region has different rules.
9. Q: What’s the shelf life of finished pellets?
A: 6-12 months if stored in a dry, well-ventilated warehouse. Use moisture-proof packaging and install dehumidifiers to avoid caking.
10. Q: How to test the quality of pellets?
A: Focus on three indicators: calorific value (≥3800 kcal/kg), mechanical strength (≥95%), and moisture content (≤15%), complying with GB/T 34229-2017 biomass pellet quality standards.
11. Q: Can I mix different raw materials for production?
A: Yes. I mix 70% corn straw and 30% wheat straw to improve calorific value, but test the ratio first to ensure molding rate.
12. Q: How to reduce electricity costs?
A: Apply for industrial electricity tariffs, use energy-efficient motors, and run the line during off-peak hours (if local electricity prices are time-of-use).

Get Your Customized Design Plan
Designing a biomass pellet line isn’t about buying the cheapest gear—it’s about building a system that works for your business, stays compliant, and makes money. I’ve wasted tens of thousands on bad design choices; every lesson here is one I paid for in cash and stress.
If you’re ready to start your biomass pellet factory and want to avoid my mistakes, contact Huaxin now. My team of engineers will craft a free, customized biomass pellet production line design for industrial use tailored to your raw materials, output goals, and budget. We handle everything from equipment picks to on-site installation and training—no guesswork, just a smooth launch.
Don’t let poor design derail your investment. Let’s build a line that’s efficient, compliant, and profitable—together.