As someone who has spent over a decade working with biomass processing equipment and dust control systems across three continents, I cannot stress this enough: dust control in your biomass pellet factory is not just about keeping your facility clean—it is about keeping your people alive and your business in operation.
I have walked through dozens of wood pellet plants, from small family-run operations to industrial-scale facilities producing hundreds of thousands of tonnes annually. And time and again, I have seen the same pattern: plants that treat combustible dust management as an afterthought inevitably pay the price. Sometimes the price is a major fire. Sometimes it is a production shutdown that costs millions. And in the worst cases—cases that still haunt me—the price is measured in human lives.
This guide draws on industry research, real-world accident investigations, and decades of practical engineering experience to give you a complete roadmap for effective dust control in your biomass pellet facility.
The Growing Demand for Dust Control in Biomass Pellet Production
The global biomass pellets market was valued at USD 14.14 billion in 2025 and is projected to reach USD 25.44 billion by 2034, growing at a CAGR of nearly 7%. As demand for renewable energy surges worldwide, more facilities are coming online, and existing plants are ramping up production. But here is the uncomfortable truth that few in this industry want to admit: every tonne of pellets you produce comes with a dust hazard that can destroy everything you have built.
The dust that biomass produces is inherently combustible. Wood dust fires and dust explosions in pellet manufacturing plants are not unusual occurrences. The finer and drier the dust particle, the lower the ignition energy required to set off an event. And in the pellet production process, you are constantly creating those ideal conditions—especially in hammer mills, dryers, conveyors, coolers, and dust collectors.
I have lost count of how many plant managers have told me, “We have been running this way for years, nothing bad has happened.” That is not wisdom—that is complacency. And complacency kills.
Real-World Lessons: What Accidents Teach Us About Pellet Mill Dust Safety
Let me share three incidents that I revisit whenever I talk about pellet mill dust safety. These are not hypothetical scenarios—they are real events.
Horizon Biofuels (Fremont, Nebraska, 2025)
On July 29, 2025, a massive explosion tore through the Horizon Biofuels facility in Fremont, Nebraska. The blast occurred when a large release of combustible wood dust ignited. The explosion fatally injured three people—an operator and his two young daughters, aged 8 and 12, who had accompanied him to work that day. The facility had a dust collection system installed. But as the investigation is still revealing, having equipment is not the same as having effective dust control.
Georgia Biomass (Waycross, Georgia, 2011)
In June 2011, one of the world‘s largest wood pellet manufacturing facilities experienced a dust explosion and resulting fire that knocked down operations for an entire month. The $175 million plant had only been open for about a month when the incident occurred, with an overheated roller/bearing assembly in a pelletizer cited as the likely ignition source. The financial impact was staggering, but the damage went beyond dollars—the explosion shattered the confidence of the plant‘s workforce and forced a complete re-evaluation of safety practices.
New England Wood Pellet (Jaffrey, New Hampshire, 2011)
The explosion and fire at this facility originated in the dust conveyor system, taking approximately 14 hours to extinguish by over 100 firefighters from 14 different departments. OSHA fined the company a total of $147,000 for safety violations including “poor dust collection system design” and “no explosion prevention / protection”.
The CSB has identified 281 combustible dust incidents between 1980 and 2005 that killed 119 workers and injured 718 more—and those numbers have only grown since. Yet the industry continues to underreport and under-learn from these tragedies.
The Science of Risk: The Dust Explosion Pentagon
To effectively control combustible dust, you need to understand what you are up against. Fire requires three elements: fuel, oxygen, and an ignition source. But a dust explosion adds two more: dispersion and confinement. These five elements together form the dust explosion pentagon.
For an explosion to occur in your pellet facility, you need:
- Fuel – Combustible biomass dust suspended in the air
- Oxygen – Present in ambient air throughout your facility
- Ignition source – A spark, hot surface, friction, static discharge, or flame
- Dispersion – Dust particles spread through the air to form a cloud
- Confinement – The dust cloud contained within a limited space
The good news is that you only need to eliminate one of these five elements to prevent an explosion. The better news is that engineering solutions exist to eliminate multiple elements simultaneously.
Biomass Dust Characteristics That Increase Hazard
Biomass dust has unique properties that make it particularly dangerous. It is lightweight, easily dispersible, and can become highly combustible when dry. Research has shown that the Kst value for wood pellet dust ranges from approximately 76 to 95 bar·m/s, indicating a significant explosion risk. The smaller the particle size, the lower the ignition energy required. Studies have also demonstrated that finer particles produce leaner MEC (Minimum Explosible Concentration) and higher values of Kst. Understanding these characteristics is essential for biomass dust hazard analysis.
High-Risk Zones in Your Pellet Manufacturing Process
From my field experience, these are the zones where you need the most vigilance:
Hammermill Systems and Particle Size Reduction Areas
This is where the danger begins. Hammermill systems and processes downstream from this step are consistently identified as the most common hazards in the biomass industry. The fine dust produced here has maximum surface area relative to volume, making it highly reactive and requiring minimal ignition energy.
Dust Collectors and Baghouses
The air-material separator (AMS) is the single most explosion-prone vessel in your entire plant. The driest and finest dust in your process stream ends up here. Adding to the threat, many pellet plants use a central dust collector that aspirates off several vessels. If an explosion occurs in that central collector, it can propagate through inlet ducts to multiple upstream vessels, causing secondary explosions.
Conveyors, Bucket Elevators and Pneumatic Transport Lines
Enclosed conveying systems can accumulate dust over time. A single spark entering a dust collection system or pneumatic line can trigger an explosion in downstream equipment or storage areas. Spark detection systems on conveyors and dust lines are essential prevention measures.
Dryers and Coolers
The heat involved in these processes combined with the presence of fine dust creates a high-risk environment. Wood pellets exiting the mill can exceed 200 degrees Fahrenheit, which is enough to ignite accumulated dust.
Storage Silos
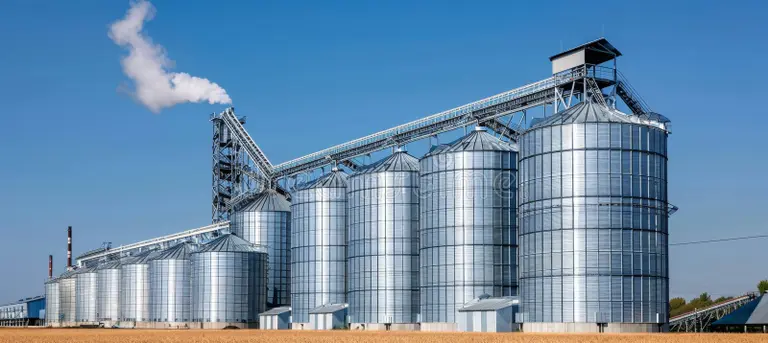
Stored biomass pellets can self-heat, creating another potential ignition source. If dust has accumulated inside a silo, you have all five pentagon elements present. Silo fire prevention requires a unique approach addressing combustible dust, structural collapse risks, and smoldering materials.
Building a Layered Safety Strategy for Dust Explosion Prevention
Here is what I have learned from helping plants across North America and Europe implement effective dust control: you need a layered approach. No single technology will solve all your problems. A layered safety approach including spark detection and explosion protection in high-risk areas is how an acceptable level of safety is achieved.
Prevention: Stop the Hazard Before It Starts
Proper Housekeeping – This is your first and most critical line of defense. A dust accumulation as thin as 1/32 of an inch (the thickness of a paper clip) can present a serious explosion hazard. Establish dust monitoring routines. Use industrial vacuums rated for combustible dust. NFPA 660 provides stricter guidance on cleaning methods, risk-based cleaning frequencies, and thresholds for dust accumulation. Never use compressed air to blow dust off surfaces—that only creates the dust cloud you are trying to avoid.
Grounding and Bonding – Proper grounding and bonding for static control is non-negotiable. Static discharge is an ignition source that many operators overlook until it is too late.
Tramp Metal Removal – Install magnetic separators to identify and remove tramp metal before it reaches your hammer mill. A single piece of metal striking a hammer can generate sparks that ignite accumulated dust.
Bearing Temperature Monitoring – Hot bearings are a common ignition source. Install monitoring systems that alert you before temperatures reach dangerous levels. Also, ensure all electrical equipment in dust-handling areas is properly rated for Class II hazardous locations.
Spark Detection and Suppression Systems
Early detection of ignition sources is the key to preventing fires and dust explosions. Spark detection and suppression systems use infrared detectors to continuously monitor material flows for hot spots, typically sparks or burning embers traveling through a duct or on a conveyor. Once detected, a water spray is injected to suppress that burning ember before it reaches downstream receiving vessels where it might find the right dust-air mix to start an explosion.
Systems like the Fagus GreCon DLD 1/9 use intelligent detection technology (IDT) to distinguish between dangerous sparks and harmless extraneous light, reducing false alarms while ensuring real threats are caught. A spark detection system is designed to lower the likelihood of an explosion occurring, but it works best when combined with other protective measures.
Explosion Protection Systems
When prevention fails—and sometimes it will—you need protection that minimizes damage.
Explosion Venting – Explosion vents are panels strategically located on the sides of baghouses or on top of cyclones. They rupture from deflagration pressures, creating an opening that releases pressure. However, vented fireballs can eject 50 feet or more, so proper siting is critical. Flame ejection calculation formulas are found in NFPA 68.
Flameless Venting – For indoor installations where free venting is not safe, flameless venting combines an explosion relief vent with a metal mesh trap that absorbs the flame and most of the heat, allowing only the overpressure to be discharged. Flameless vents from manufacturers like IEP Technologies are available for conveyors as well.
Chemical Suppression – Explosion suppression systems detect the incipient deflagration and, within milliseconds, inject a dry chemical extinguishing agent into the protected vessel to suppress the explosion before damaging pressure buildup can occur.
Explosion Isolation – Explosion isolation devices prevent flame and pressure from propagating through ductwork to other parts of your facility, containing the event to a single vessel.
Dust Hazard Analysis (DHA)
A dust hazard analysis (DHA) should be conducted to identify areas of risk within your facility and indicate strategies to minimize the potential for an explosion during normal operating and upset conditions. NFPA standards require that a DHA be completed for any new processes handling combustible dust and must be updated every five years.
Regulatory Compliance: NFPA 660 and Beyond
I cannot emphasize this enough: regulatory compliance is not optional. It is the minimum standard of care you owe your workers and your community.
What Is NFPA 660?
Effective December 6, 2024, NFPA 660: Standard for Combustible Dusts and Particulate Solids replaced six separate combustible dust standards (61, 484, 652, 654, 655, and 664) into one comprehensive framework. The new standard was developed by well over 100 expert individuals and provides a unified, single-source document for industries managing combustible dust and particulate solids.
NFPA 660 provides a comprehensive framework for safer work environments by preventing dust-related fires and explosions. Key requirements include:
- Identification and classification of combustible dust hazards
- Engineering and administrative controls
- Employee training to recognize dust hazards and follow safe operating procedures
- Interim safeguards when full compliance cannot be immediately achieved
NFPA 664 for Wood Processing Facilities
NFPA 664, Standard for the Prevention of Fires and Explosions in Wood Processing and Woodworking Facilities, is the controlling document for protecting wood biomass and wood pellet plants from wood dust. It offers comprehensive criteria for designing, operating, and protecting facilities that process wood or manufacture wood products.
OSHA and CSB Enforcement
OSHA has fined multiple wood pellet facilities for combustible dust violations. For facilities in China, note that biomass boiler emission limits are regulated under GB13271-2014, requiring particulate matter concentrations below 50mg/m³ (standard limits) or 30mg/m³ (special emission limits). Several provinces have implemented even stricter local standards.
Why Pulse Jet Baghouse Dust Collectors Are the Industry Standard
After reviewing hundreds of dust control installations, I can tell you that pulse jet baghouse dust collectors have become the industry standard for biomass pellet plants—and for good reason.
How Baghouse Dust Collectors Work
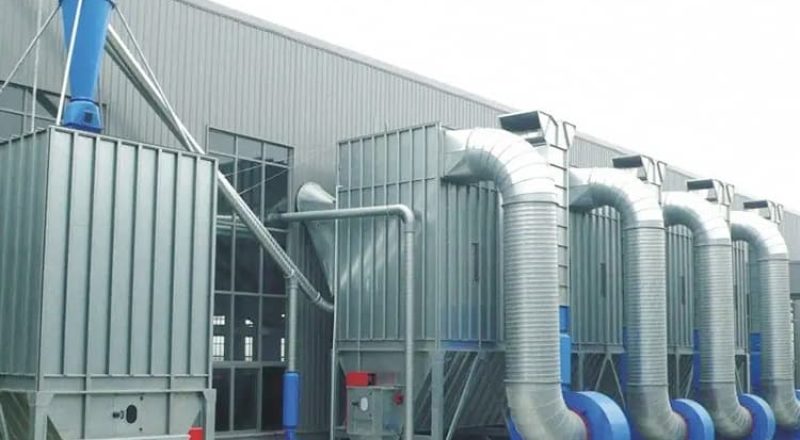
Biomass dust collection is designed to capture and remove airborne particles generated during processing, handling, or storage. A baghouse system filters out and collects the dust particles from the airstream using various filtration media. As the dust-laden air passes through the filter media, dust particles are trapped and accumulate on the filter surface, while clean air is discharged into the atmosphere.
A pulse jet baghouse uses compressed air pulses to periodically clean the filter bags, maintaining low pressure drop and continuous operation. When properly specified and maintained, these systems achieve filtration efficiency exceeding 99.9%, effectively controlling PM2.5 and even finer particulate emissions.
Filter Media Selection for Biomass Dust
For biomass applications, filter media must offer high separation efficiency, good chemical resistance, and resistance to high process humidity. Recommended materials include anti-static, oil-repellent, and moisture-repellent coated filter fabrics. Filtration velocity is typically controlled at 0.8–1.2 m/min depending on dust concentration and characteristics, with filter area reserved to accommodate process fluctuations. The best systems incorporate explosion protection as standard: spark detection devices, flame arrestors, explosion venting or flameless venting, and flame-retardant filter media.
Engineering Design Best Practices
A complete biomass dust collection system typically consists of collection hoods, ductwork networks, the dust collector itself, fans, discharge devices, and control systems. The design philosophy centers on “source capture, air volume matching, efficient separation, and safe emissions.”
I recommend a “cyclone + baghouse” two-stage combination for biomass dust characteristics. The cyclone separator acts as pretreatment, removing most coarse particles and reducing the load on the baghouse. Ductwork should minimize elbows and maintain reasonable air velocity (typically 12–18 m/s) to prevent dust deposition.
The collected dust can often be recycled back into the production process as fuel, reducing waste and improving overall plant economics.
Practical Steps You Can Take Tomorrow
If you take only five actions from this guide, let these be them:
- Conduct a dust hazard analysis for every area of your plant where combustible dust is generated or accumulates
- Establish a daily housekeeping protocol that includes documented dust level checks using calibrated inspection tools
- Verify that all your electrical equipment in dust-handling areas is properly rated for hazardous locations
- Test your spark detection and suppression systems monthly—not just annually
- Train every employee on the dust explosion pentagon and the specific ignition sources relevant to their workstations. NFPA 660 requires that employees are trained to recognize dust hazards and follow safe operating procedures
A Final Word from the Field
I have stood in the wreckage of a pellet plant that had a “good” safety record—right up until the day it did not. The operator who lost his life had worked there for fifteen years. He knew the plant better than anyone. And he still died because a layer of fugitive dust in a location nobody checked became a fuel source for an explosion that no single safety system could contain.
Do not let your plant become another statistic.
The technology exists to make biomass pellet production safe. The standards exist to guide you. The only missing piece is the commitment to implement both correctly and consistently.
Frequently Asked Questions
Q1: What is the most dangerous area for dust accumulation in a biomass pellet factory?
The hammermill system and its downstream processes consistently pose the highest risk due to the fine particle size and high dispersion potential of the dust produced. Dust collectors and baghouses are the next most vulnerable vessels, with the air-material separator (AMS) being the single most explosion-prone vessel in the entire plant.
Q2: How often should I conduct a dust hazard analysis (DHA) at my facility?
NFPA standards require a DHA for any new processes handling combustible dust, and it must be updated every five years. A full DHA should be conducted with ongoing hazard assessments integrated into your routine safety inspections.
Q3: Can I use compressed air to clean dust off surfaces in my plant?
No. Never use compressed air to blow dust off surfaces. This disperses accumulated dust into the air, creating a dust cloud that may exceed explosive concentration limits. Use industrial vacuums specifically rated for combustible dust.
Q4: What is the difference between explosion venting and flameless venting?
Explosion venting releases pressure and a fireball through a rupture panel, requiring a safe outdoor discharge area. The fireball can eject 50 feet or more. Flameless venting uses a metal mesh trap to absorb the flame and most heat while releasing only overpressure, making it suitable for indoor installations.
Q5: How do spark detection systems protect my facility?
Spark detection systems use infrared sensors to continuously monitor material flows for high-temperature particles. When a spark or ember is detected, the system automatically activates water extinguishing nozzles downstream, preventing the ignition source from reaching dust collectors or storage areas.
Q6: What dust layer thickness is considered a hazard?
A combustible dust accumulation of just 1/32 of an inch (about the thickness of a paper clip) can present a serious explosion hazard. Any visible dust accumulation should be addressed immediately through proper housekeeping protocols.
Q7: What is NFPA 660, and why does it matter for my pellet plant?
Effective December 6, 2024, NFPA 660 replaced six separate combustible dust standards into one consolidated framework. It provides a unified, single-source document for industries managing combustible dust and particulate solids, with stricter guidance on cleaning methods, risk-based cleaning frequencies, and engineering controls.
Q8: How efficient are modern biomass dust collection systems?
High-quality pulse jet baghouse dust collectors achieve filtration efficiency of 99.9% or higher, effectively controlling PM2.5 and finer particulate emissions while meeting stringent environmental compliance standards. When properly integrated with cyclone pre-separators, systems can achieve outlet dust concentrations below 10mg/m³.
Q9: What regulatory standards apply to dust control in wood pellet manufacturing?
Key standards include NFPA 660 (consolidated combustible dust standard), NFPA 664 (wood processing facilities), NFPA 68 (explosion venting), and for international facilities, local emission standards such as GB13271-2014 in China.
Q10: What is the best dust control solution for existing pellet plants?
For existing facilities, a layered approach combining daily housekeeping protocols, localized dust collection upgrades, and retrofitted spark detection systems typically delivers the fastest safety improvements without requiring complete plant redesign.
Q11: Where can I find a comprehensive dust control guide for pellet factory operations?
Facility managers should start with the NFPA website for standards documentation (NFPA 660 and NFPA 664) and consult qualified safety engineers for site-specific dust hazard analysis and system design.
Q12: What is the role of flame-retardant filter media in biomass dust control?
Flame-retardant filter media are designed to prevent filter bags from igniting if sparks or embers reach the dust collector. This is a critical safety feature for pulse jet baghouse systems handling combustible wood dust.
Ready to Protect Your Facility and Your People?
Do not wait for an incident to force your hand. Whether you need a complete dust control system for a new plant, a retrofit for existing equipment, or a site-specific dust hazard analysis, we are here to help.
Contact Huaxie Machinery today for:
- Custom dust collection system design tailored to your facility layout and production volume
- Pulse jet baghouse dust collectors with explosion protection features
- Complete dust hazard analysis and NFPA compliance consulting
- Spark detection and suppression system integration
- Professional installation, training, and ongoing technical support
Your facility‘s safety is our priority. Let us help you build a dust control strategy that works—not just on paper, but on every shift, every day of the year.