Over the past twelve years at Huaxin Machinery, I have stood beside hundreds of biomass pellet mills during their first startup, watched operators struggle with inconsistent pellet density, and celebrated when a stubborn batch of rice husk finally compressed into uniform cylinders. If there is one thing I have learned, it is this: understanding the biomass pellet mill working principle is not just academic—it directly determines your yield, your power consumption, and whether your pellet mill die and roller last six months or six weeks.
This article breaks down exactly what happens inside that compression chamber, why lignin behaves like nature’s glue under heat, and how the choice between ring die pellet mill and flat die pellet mill changes everything about your pellet production line.

What Actually Happens Inside a Pellet Mill?
At its core, a biomass pellet mill is a high-pressure extrusion machine. Raw material—typically ground to particles under 3 mm—is forced through cylindrical holes in a metal die by rotating rollers. That sounds simple, but the physics inside the chamber are surprisingly sophisticated.
When rollers press biomass against the die, friction generates temperatures between 90°C and 120°C. At this heat, the natural lignin inside woody or fibrous material begins to soften. Lignin is an amorphous polymer with no fixed melting point, but its adhesive properties start increasing around 70°C and reach optimal binding strength between 140°C and 200°C. This lignin binding mechanism means the pellet holds together not because of any added glue, but because the material’s own chemistry activates under mechanical stress and thermal energy.
The result is a cylindrical pellet with a density typically rising from 100–150 kg/m³ as loose sawdust to 600–700 kg/m³ as finished fuel. That densification is what makes biomass fuel pellets economically viable for transport and combustion.
Ring Die vs. Flat Die: Two Different Philosophies
If you are sourcing wood pellet machine equipment, you will encounter two dominant designs. Their working principles differ in ways that affect capacity, maintenance cycles, and raw material tolerance.
Ring Die Pellet Mills
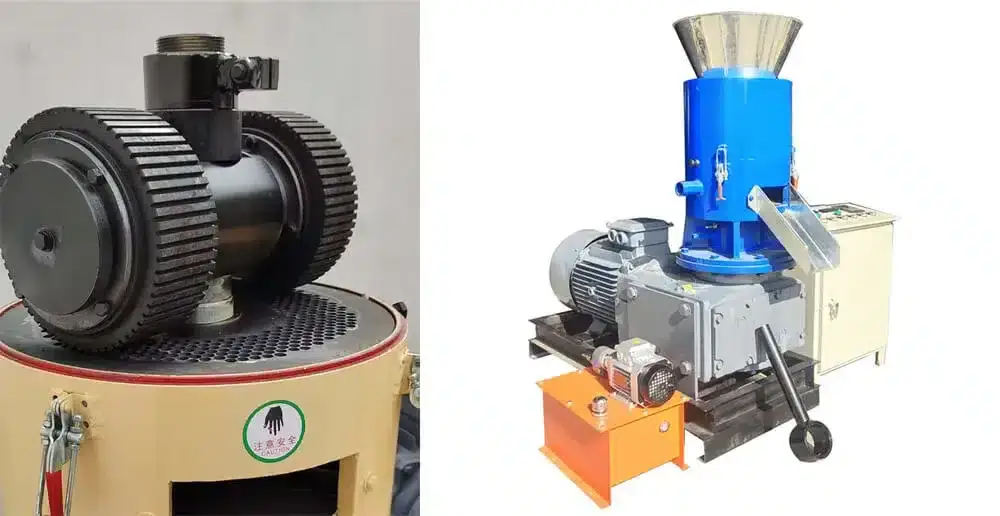
In a ring die pellet mill configuration, the die itself rotates at high speed while rollers remain stationary relative to the die’s inner surface. Material enters through a forced feeder, gets distributed by centrifugal force against the inner die wall, and is compressed outward through the holes.
This design excels in continuous industrial operation. The centrifugal distribution ensures even material spread, and the multiple roller sets—usually two or three—create sustained high pressure. Industrial pellet mills in ring die configuration typically handle 500 kg/hour to over 5 tons/hour. They are the standard for commercial pellet mills processing hardwood, straw, or mixed agricultural waste.
However, the complexity comes with trade-offs. Ring die pellet mills require precise pellet mill die and roller gap adjustment—usually 0.1 to 0.3 mm—and the forced feeder must match the material’s flow characteristics. Get the gap wrong, and you either get “washthrough” (uncompressed material pouring through the die) or catastrophic clogging that stalls the main motor.

Flat Die Pellet Mills
Flat die pellet mills invert the geometry. A horizontal flat die plate stays stationary or rotates slowly, while rollers above it spin and press material downward through the holes. Gravity does the initial feeding, which makes the design elegantly simple.
These machines suit small scale pellet mill operations—farms, workshops, or mobile production units. Capacities range from 80 kg/hour to around 1,000 kg/hour. The open design allows operators to see material behavior in real time, and pellet mill maintenance—cleaning die holes, adjusting roller clearance—can often be done without lifting equipment.
The limitation is pressure consistency. Because material feeds by gravity, soft or irregularly sized biomass can create uneven density across the die surface. Flat die pellet mills work beautifully with sawdust and finely ground straw, but struggle with long-fiber materials like palm fronds or wet corn stalks unless pre-processed aggressively.
The Pre-Treatment Chain: Why Pellet Quality Is Decided Before the Mill
Here is something most pellet mill manufacturer brochures gloss over: the pellet mill is only the final stage of a complete pellet production line. What happens upstream determines whether the machine performs or fails.
Size reduction comes first. Standard wood pellet machines require feedstock ground to 3 mm or smaller. Large wood chunks must pass through a chipper, then a hammer mill. Agricultural residues like wheat straw can sometimes skip chipping if the hammer mill has sufficient power, but uniform particle size is non-negotiable. Uneven material creates pressure spikes that crack dies and overload bearings.
Moisture control is the silent killer of productivity. For most woody biomass, 10–15% pellet mill moisture content is the sweet spot. Above 20%, steam forms inside the die holes, causing pellets to expand and crumble upon exit. Below 8%, lignin does not soften adequately, and pellets emerge fragile or fail to form at all. In my experience, operators who skip the dryer and feed wet sawdust directly into the sawdust pellet machine end up with a die clogged within two hours and a maintenance bill that erases a week of profit.
Some materials need conditioning. Steam injection before the biomass pellet mill can raise moisture slightly in overly dry material and pre-heat the biomass to reduce the mechanical load on the rollers. For feed pellets, this step is standard; for fuel pellets, it depends on the raw material’s starting condition.
Critical Process Parameters Operators Must Monitor
Once material enters the compression chamber, three variables govern output quality:
Temperature. The die and roller friction must generate enough heat to plasticize lignin without scorching the material. If the pellet press machine runs too cold—usually because the feed rate is too low or the material is too wet—pellets lack cohesion. If it runs too hot, the die surface can glaze, reducing friction and causing slip.
Pressure and roller gap. The gap between roller and die determines how much material gets grabbed and compressed. A gap that is too wide causes low density and washthrough. Too narrow, and the rollers grind against the die, accelerating pellet mill die wear and generating excessive heat. We typically recommend checking the gap every 40 operating hours and recalibrating after die changes.
Die hole specifications. Hole diameter—commonly 6 mm or 8 mm for fuel pellets—determines pellet size. But the pellet mill compression ratio (the length of the tapered inlet section relative to the straight section) is equally important. Hardwoods like oak need a lower compression ratio because their dense fiber structure already provides natural binding. Soft, fluffy materials like rice husks need higher compression ratios to achieve equivalent density.
Common Failures and How to Read Them
After pellet mill troubleshooting for thousands of calls from clients, I can usually diagnose a problem by asking what the failed pellets look like.
Powdery, crumbling pellets almost always mean insufficient lignin activation. Check moisture first, then temperature. If the wood pellet machine is new, the die might need “running in”—a break-in period where the micro-roughness of fresh steel holes optimizes friction.
Long, irregular strands instead of clean cylinders suggest dull or improperly set cutters beneath the die. The slicer blade must sit at the correct distance from the die face; even a 2 mm misalignment creates ragged ends that break during conveying.
Sudden motor overload or jamming usually indicates foreign matter—stones, metal fragments, or oversized material—entering the chamber. A magnetic separator upstream and a properly sized hammer mill screen prevent 90% of these incidents.
Pellets with cracked radial surfaces exiting the die too hot and cooling too fast. Slow down the cutter, check cooling air flow, or reduce throughput slightly to let heat dissipate more evenly.
Maintenance Reality: What Extends Die Life
A ring die pellet mill die for an industrial setup represents a significant capital expense. Yet I see operators ruin dies in three months through neglect. The fundamentals are not complicated, but they require discipline.
Automatic lubrication systems are standard on modern industrial pellet mills for good reason. The main shaft bearings, roller bearings, and gearbox all need timed grease delivery. Skipping lubrication causes metal-on-metal contact that generates heat, distorts the die, and creates vibration that propagates through the entire drive train.
Pellet mill die and roller cleaning matters. When production stops, residual biomass in the holes hardens like cement. Before the next startup, run a small amount of oily material—sometimes we use a mix of fine sawdust and vegetable oil—through the biomass pellet machine to flush and condition the holes. For severe blockages, a drill-specific cleaning tool is necessary; never hammer on the die face.
Finally, monitor pellet mill die wear patterns. Uneven wear across the die circumference indicates uneven material distribution, often caused by a misaligned feeder or worn roller shells. Catching this early allows you to adjust the feeder or rotate the die before the damage becomes irreversible.

Why This Matters for Your Operation
Understanding the biomass pellet mill working principle is not about memorizing a mechanical sequence. It is about recognizing that every variable—pellet mill moisture content, particle size, die geometry, roller pressure—interacts in a system. Optimize one element while ignoring the others, and you get subpar pellets at higher cost.
At Huaxin Machinery, we have built our reputation not just on manufacturing renewable energy equipment, but on helping clients understand these interactions. Whether you are processing pine sawdust in a 500 kg/hour flat die pellet mill setup or running a 3-ton-per-hour ring die pellet mill line on mixed agricultural waste, the physics remain the same. Master them, and your pellets become a consistent, profitable fuel source.
Frequently Asked Questions
A biomass pellet mill compresses ground raw material through holes in a die using rotating rollers. Friction generates heat that softens natural lignin, which binds the particles into dense pellets without added adhesives.
Ring die pellet mills use a rotating cylindrical die with internal rollers for high-capacity continuous production. Flat die pellet mills use a horizontal stationary die with overhead rollers, offering simpler pellet mill maintenance and lower cost for small scale pellet mill operations.
Common materials include wood sawdust, wood chips, straw, rice husks, peanut shells, palm shells, corn stalks, bark, and other agricultural or forestry residues. A rice husk pellet mill or straw pellet machine handles specific agricultural waste streams.
For most woody biomass, 10–15% pellet mill moisture content is optimal. Too much moisture causes poor binding and die clogging; too little prevents lignin from activating as a natural binder.
Generally no. The lignin naturally present in woody biomass softens under heat and pressure, acting as an effective binder. Only certain low-lignin materials like pure grass may require additives.
This usually results from excessive moisture, insufficient compression temperature, or worn die holes. Check your raw material moisture and verify that the wood pellet machine is reaching adequate operating temperature.
Clogging typically occurs from overly wet material, excessive feed rate, foreign objects, or rollers set too close to the die. A properly sized hammer mill and magnetic separator upstream prevent most jams.
Inspect pellet mill die and roller gap every 40 operating hours. Die lifespan varies by material abrasiveness but typically ranges from 800 to 1,500 hours for quality alloy dies. Replace rollers when surface wear exceeds 2 mm.
Yes, for small to medium output. However, for continuous 24-hour industrial production exceeding 1 ton per hour, a ring die pellet mill offers better durability, energy efficiency, and automation.
Pellet mill compression ratio ranges from 1:4 to 1:6 depending on material density. Hardwoods use lower ratios; soft, bulky materials like straw or rice husk require higher ratios to achieve sufficient pellet density.
The friction-generated temperature must reach 90–120°C to soften lignin adequately. Insufficient heat produces weak pellets; excessive heat can glaze the die surface and reduce extrusion efficiency.
For commercial pellet mill fuel production, ring die pellet mills starting at 1 ton per hour are standard. Match pellet mill capacity to your raw material supply, drying capacity, and downstream cooling and packaging systems.
Ready to Optimize Your Pellet Production?
Whether you need a complete pellet production line or expert guidance on die selection and raw material preparation, our engineering team is ready to help. With over a decade of hands-on experience in biomass pellet machine manufacturing, Huaxin Machinery delivers reliable ring die pellet mills and flat die pellet mills tailored to your specific feedstock and capacity requirements.
Contact us today for a free consultation, detailed wood pellet machine for sale quotation, or customized pellet production line design. Let us turn your agricultural and forestry waste into profitable, sustainable energy production.