After spending over a decade working with biomass pellet production lines across Asia and Europe, I have come to one clear conclusion: bonding technology is the invisible backbone of every high-quality pellet. You can have the best raw material, the most expensive die, and perfect moisture content, but if the inter-particle bonding fails, your pellets will crumble before they ever reach the boiler.
In this article, I want to share what I have observed firsthand about biomass pellet bonding technology—the mechanisms that actually hold pellets together, the variables that make or break pellet durability, and why this topic deserves far more attention than it typically gets on the factory floor.
What Biomass Pellet Bonding Technology Actually Means
When we talk about biomass pellet bonding technology, we are referring to the physical and chemical forces that bind compressed biomass particles into a stable, durable pellet. These forces are not created by adding glue in the traditional sense. Instead, they emerge from the biomass itself under the right combination of heat, pressure, and moisture.
From my experience running pilot-scale tests with corn straw, rice straw, peanut shells, and hardwood sawdust, I have seen how dramatically bonding behavior changes depending on the feedstock. Research published in Agriculture confirms this: under standard biomass densification conditions (298 K, 60–1500 N, 10 s dwell time, <0.5 mm particle size, 10% moisture), corn straw pellets showed strong bonding with no visible cracks, while camphor leaf pellets remained soft and prone to loosening. The difference lies in the intrinsic composition of each biomass type.

The Four Core Pellet Bonding Mechanisms
Through both field observation and literature review, I categorize biomass pellet bonding into four dominant mechanisms. Understanding these has helped me troubleshoot countless pellet production issues.
1. Lignin Softening and Solid Bridging
Lignin is, without question, the most important natural binder for wood pellets. When temperature and pressure are applied during pelletizing, lignin transitions from a glassy state into a plastic, flowable form. It then extrudes from cell walls, fills gaps between particles, and hardens upon cooling to create what researchers call “solid bridges.”
I have noticed this effect most clearly when comparing hardwood branches (high lignin) with herbaceous grasses (low lignin). The hardwood pellets consistently show higher relaxation density and pellet durability because the lignin content creates more solid bridges between particles. This is why lignin pellet binder performance is so critical when selecting feedstock for biofuel pellet production.
2. Mechanical Interlocking
Long fibers in biomass materials such as rice straw and hardwood branches intertwine during compression, forming a network structure that resists fracture forces caused by elastic rebound. In my own tests, I have observed that materials with longer fibers require higher compression energy but produce pellets with superior shear resistance and compression strength.
3. Hydrogen Bonding and Van der Waals Forces
At the molecular level, when surfaces rich in hydroxyl groups are pressed together, multiple hydrogen bonds form among adjacent particles. Under certain conditions, dehydration can even create covalent bonds such as ethers and esters, cross-linking the surfaces. These weaker forces become significant only when particles are in extremely close contact—something that proper particle size and compression pressure must achieve first.
4. Weak Boundary Layer Disruption
Here is a lesson I learned the hard way: not all biomass surfaces are ready to bond. Straw materials, for instance, contain high levels of extractives concentrated on the outer cuticle. These hydrophobic compounds create a weak boundary layer that prevents stable bond formation. I once saw an entire batch of straw pellets fail durability tests simply because the raw material had not been pre-treated to remove surface waxes.
Critical Process Parameters That Control Pellet Bonding
Through trial and error on industrial biomass pellet machine production lines, I have identified four non-negotiable variables:
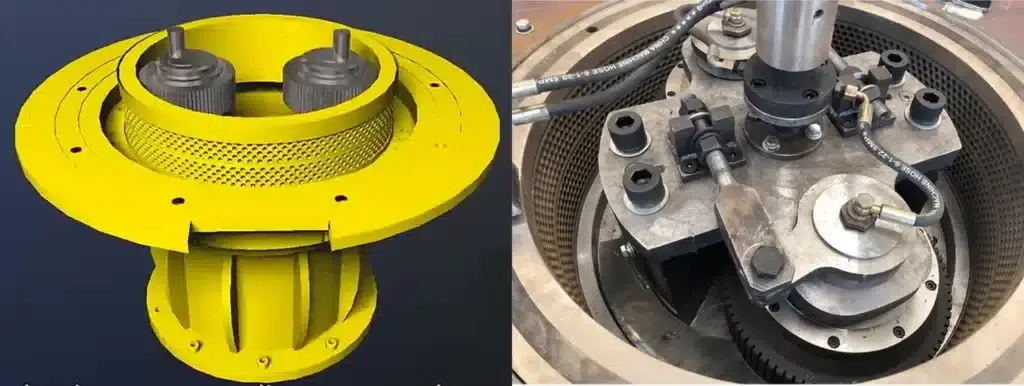
Die Temperature: The die temperature typically ranges between 100 °C and 130 °C, with pressure between 115 MPa and 300 MPa. Below this range, lignin does not soften sufficiently. Above it, you risk excessive energy consumption and equipment wear.
Moisture Content: I generally target 8–12% moisture content for optimal biomass pellet bonding. Too little moisture, and hydrogen bonding suffers; too much, and you get steam expansion cracks during cooling.
Particle Size: My rule of thumb is to keep particle size below 0.5 mm for uniform compaction. Larger particles create voids and weak points that reduce pellet density.
Compression Pressure: Higher pressure increases particle contact area and promotes lignin flow, but there is a ceiling. Beyond optimal pressure, the energy cost rises faster than the bonding benefit.
When Natural Bonding Is Not Enough: Organic Binders for Biomass Pellets
In some cases—especially with torrefied biomass or herbaceous materials with high extractive content—natural bonding is insufficient. This is where organic binders enter the picture.
Research from the University of Science and Technology Beijing has systematically reviewed biomass-based organic binders such as lignosulfonate, carboxymethyl cellulose (CMC), and carboxymethyl starch (CMS). These binders rely on chemical adsorption of carboxyl groups and hydrogen bonding of hydroxyl groups to enhance pellet strength. From a practical standpoint, I have found that adding 1–3% lignosulfonate can improve pellet durability by 15–25% for low-lignin feedstocks.
However, the main challenge remains high-temperature strength loss during combustion, which is why current research is exploring composite additives like LD sludge and nano-CaCO₃ to overcome this limitation. If you are evaluating organic binder vs bentonite for pellets, the key advantage of organic options is their renewability and lower ash content.
Biomass Pretreatment: The Overlooked Bonding Enhancer
Before pellets even reach the die, biomass pretreatment can fundamentally alter bonding potential. Steam treatment at 180–240 °C ruptures cellular structures and loosens lignin bonds, making the material more amenable to compression. Acid or alkali treatments can also modify the lignocellulosic matrix, though these require careful handling due to corrosion and effluent concerns.
In my own facility, we have seen torrefied biomass pellets—which inherently lose some lignin bonding capacity during thermal treatment—respond well to binder addition. The severity of torrefaction directly correlates with how much additional binder is needed to maintain pellet quality.
Common Pellet Production Challenges I Have Encountered
Let me be direct about the problems I have faced on the wood pellet production line:
- Layering in straw pellets: Rice straw pellets often show a layered cross-section with fillers acting as solid bridges between layers. This reduces shear resistance and pellet durability.
- High energy consumption with hard shells: Peanut shells, despite excellent bonding, consumed up to 61,160 J/kg in our tests due to their hard texture and stable structural composition.
- Hydrophobic extractives: Herbaceous crops with high fat and wax content form a polyester keratin layer on particle surfaces, reducing interactions and preventing solid bridge formation.
The Future of Sustainable Pellet Production Technology
I believe the next five years will bring two major shifts. First, molecular-level optimization of organic binders—specifically increasing the degree of substitution of functional groups and overall polymerization—will allow these materials to fully replace traditional bentonite in industrial applications. Second, composite binders combining biomass derivatives with industrial solid wastes will solve both the high-temperature strength problem and the waste disposal challenge simultaneously.
Frequently Asked Questions
1. What is biomass pellet bonding technology?
It refers to the physical and chemical mechanisms—such as lignin softening, hydrogen bonding, and mechanical interlocking—that bind compressed biomass particles into durable pellets without requiring external adhesives.
2. Does biomass pellet production require added glue or chemical binders?
Not always. Many wood pellets rely entirely on natural lignin as a binder. However, low-lignin or torrefied materials often benefit from organic binders like lignosulfonate or CMC.
3. What role does lignin play in pellet bonding?
Lignin softens under heat and pressure, flows between particles, and hardens upon cooling to form solid bridges. It is the primary natural binder in lignocellulosic biomass.
4. Why do straw pellets have lower pellet durability than wood pellets?
Straw contains high levels of hydrophobic extractives (waxes and fats) on its outer surface, which create a weak boundary layer that interferes with inter-particle bonding.
5. What is the ideal moisture content for biomass pellet bonding?
Generally 8–12% by weight. This range balances the need for hydrogen bonding with the risk of steam-induced cracks during cooling.
6. How does die temperature affect bonding strength?
A die temperature of 100–130 °C is typical for biomass densification. It softens lignin and reduces friction, but excessive heat can degrade biomass polymers or increase energy consumption.
7. What are organic binders for biomass pellets, and when should they be used?
Organic binders such as lignosulfonate, CMC, and CMS are derived from renewable biomass. They are recommended for feedstocks with low natural lignin or for torrefied biomass pellets where native bonding capacity has been reduced.
8. Can torrefied biomass be pelletized without binders?
Severely torrefied biomass generally produces poor-quality pellets without binders because the torrefaction process degrades the lignin responsible for natural bonding.
9. What particle size is best for strong pellet bonding?
Particles smaller than 0.5 mm generally produce the best results, as they increase contact area and allow more uniform compression.
10. How does biomass pretreatment improve pellet bonding?
Steam, acid, or alkali pretreatments rupture cellular structures and loosen lignin bonds, making the biomass more compressible and improving natural bonding potential.
11. What causes pellets to crack or crumble after pellet production?
Common causes include insufficient lignin content, excessive moisture, inadequate compression pressure, or the presence of hydrophobic extractives that prevent proper inter-particle contact.
12. How can I test the bonding quality of my biomass pellets?
Standard methods include durability testing (tumbling), compression strength testing, and scanning electron microscopy (SEM) analysis of fracture surfaces to observe fiber pullout and polymeric flow.
Ready to Optimize Your Pellet Bonding Process?
If you are struggling with pellet durability, high energy consumption, or inconsistent feedstock quality, the solution often lies in refining your bonding strategy—not just buying a bigger motor. At Huaxin, we have spent years analyzing how raw material chemistry, die design, and process parameters interact to determine pellet quality.
Contact Huaxin today for a free technical consultation. Whether you need biomass pellet machine recommendations, binder selection guidance, or a complete custom pelletizing solution tailored to your biomass type, our engineering team is ready to help you produce high-durability biomass pellets that meet the highest international standards.